CUSTOM TENT BUYER GUIDE
Clean Manufacturing Overflow Tent: Capacity Planning Guide
Plan a clean manufacturing overflow tent around process boundaries, zoning, utilities, contamination risk, validation and change control.
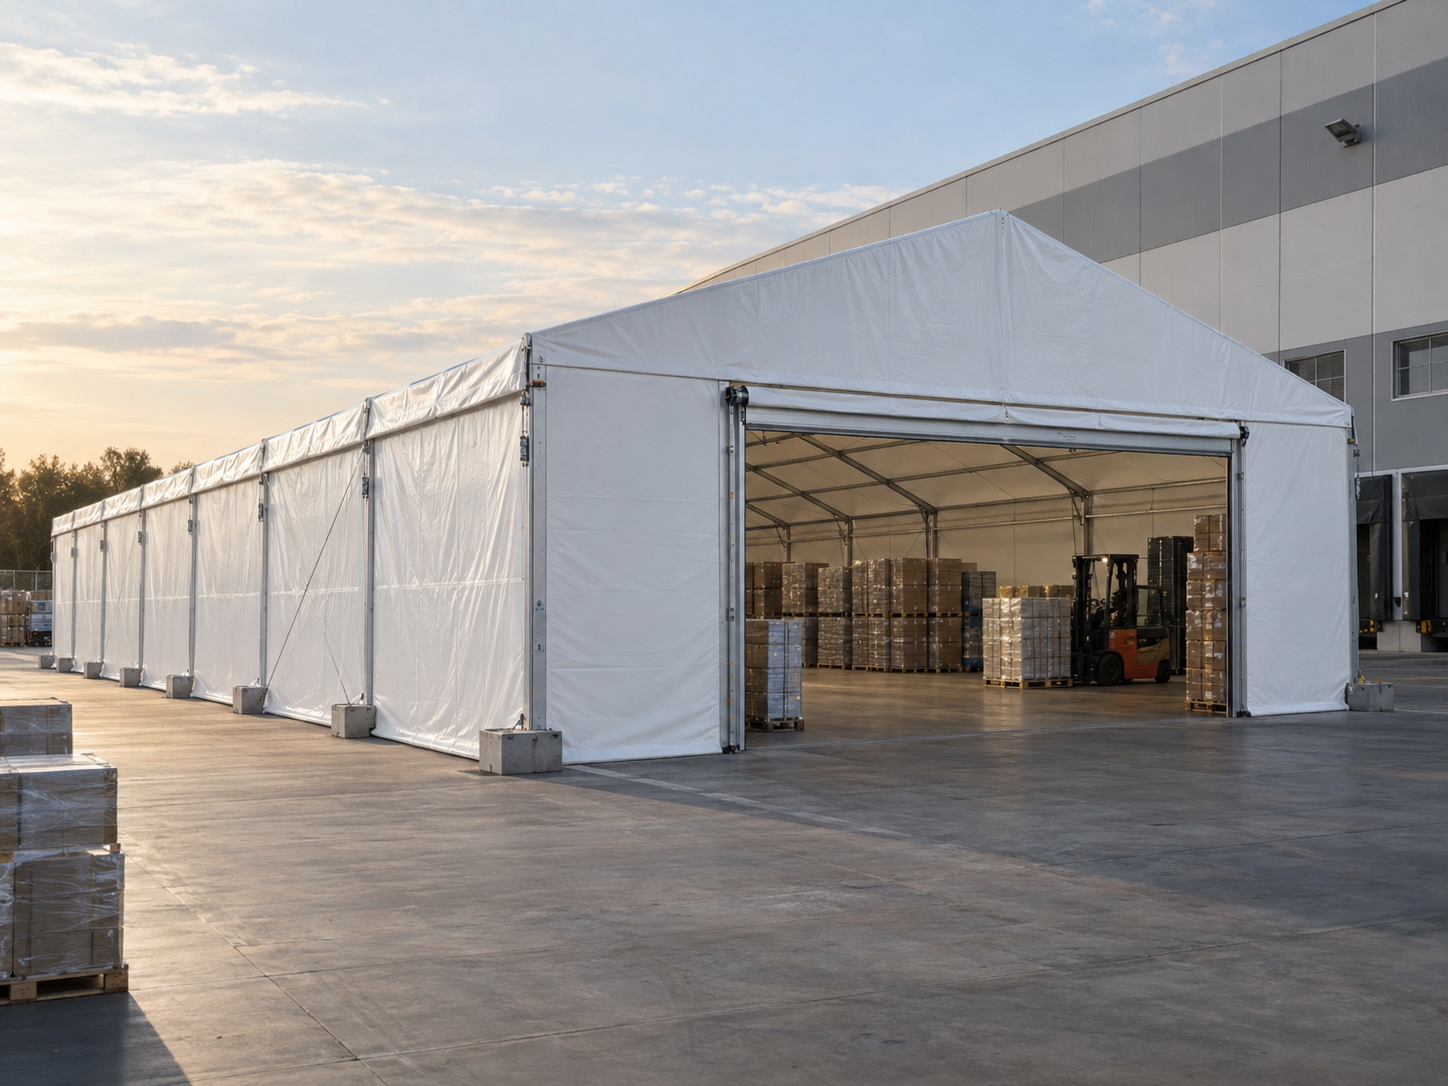
- Introduction
- Quick answer
- Buyer takeaways
- Define the operating requirement before selecting a tent
- Survey the site and movement envelope
- How to specify a clean manufacturing overflow tent
A buyer searching for a clean manufacturing overflow tent is not simply looking for fabric and a frame. The real requirement is adding temporary protected capacity for a clearly bounded assembly, inspection or material-support process. This guide is written for operations leaders, quality teams, facility engineers, contract manufacturers and capital procurement teams. It explains how to define the operating boundary, survey the site, compare suppliers, plan inspection and prepare the enclosure for safe handover without treating a temporary tent as a substitute for process engineering.
Related searches such as temporary clean production enclosure, controlled manufacturing expansion tent, clean assembly overflow space, modular contamination control tent show the same commercial intent from different angles. They are addressed naturally rather than repeated as slogans. Every example below is a procurement scenario, not a claim that TentDawn completed a named customer project. TentDawn's 8,000 m² Shenzhen factory is user-provided company information; factory testing and shipment inspection must be agreed for each actual purchase order.
Quick answer
Specify the controlled manufacturing overflow enclosure from the operation outward. Freeze the largest equipment envelope, people and vehicle routes, environmental limits, utility interfaces, site hazards, structural basis and acceptance evidence before approving price. The tent supplier can manufacture the agreed enclosure, but the process owner and quality organization control classification, contamination limits, validation, utilities, training and product release. A useful RFQ makes that division visible.
For a fast first review, ask whether the proposed layout can support running one representative material-and-personnel flow without crossing dirty receipt, waste or rejected-product routes. If the answer depends on an unmeasured opening, assumed ground condition or undocumented utility load, the proposal is not ready for production release.
Buyer takeaways
- Define the exact process and cleanliness objective before discussing the building.
- Separate material, personnel, waste and maintenance routes.
- Treat filtration, pressure and environmental control as engineered process systems.
- Validate the installed arrangement before product enters.
- Use formal change control when products, volumes or utilities change.
Define the operating requirement before selecting a tent
Map the real workflow
For the controlled manufacturing overflow enclosure, begin with mapping material receipt, gowning if required, protected entry, assembly or inspection, in-process hold, release, waste and cleaning. Draw the sequence from arrival through isolation, handling, work or storage, quality release and exit. Mark where weather, contamination, congestion or a delayed handoff could damage the asset or interrupt the schedule. This process map should control the floor plan; a catalogue width should not control the process.
List the tools, consumables, waste, spares and documentation that move with the main asset. Include carts, fixtures, packaging, rejected items, cleaning tools and maintenance access so temporary capacity does not create uncontrolled shortcuts. Distinguish normal operation from exceptional states such as a failed component, quarantine, rework, emergency evacuation or peak-volume day. Those exceptional states often determine the useful door position and spare floor area.
Assign responsibilities and exclusions
The owner should identify who controls process validation, quality release, contamination control, EHS, cleaning, utilities, training and deviation handling. The tent supplier should state its design assumptions, supplied components, factory checks, packaging scope and installation support. Site civil work, regulated equipment, process ventilation, electrical distribution, fire strategy and operational permits remain with the appointed specialists unless the contract explicitly assigns them.
Create a responsibility matrix with one owner for every interface. For this controlled manufacturing overflow enclosure, the matrix should include existing plant, transfer vestibules, floor, HVAC or filtration, power, data, fire systems, security and waste. An empty cell is not a shared responsibility; it is an unresolved project risk.
Survey the site and movement envelope
Record geometry and access in operating position
Measure equipment footprints, operator positions, cart routes, maintenance pull space, transfer doors and separated material or personnel entries. Record both outside dimensions and clear usable dimensions after door tracks, bracing, liners, thresholds and tolerances. Model the worst movement, not the easiest: moving protected work-in-progress from the permanent facility into the overflow space without crossing incoming waste or construction traffic. Include delivery vehicles, lifting equipment and temporary erection zones on the same controlled drawing.
Confirm overhead restrictions, buried services, slopes, drainage routes and adjacent operations before selecting anchoring. The controlled manufacturing overflow enclosure may fit the final footprint but still fail logistics if the longest package cannot reach the site, the crane cannot deploy or an exit route crosses the work zone.
Capture environmental and location inputs
Document particles, temperature, humidity, condensation, construction dust, pest entry, drainage and cleaning chemistry. Use location-specific wind, snow, seismic, flood, corrosion and ground inputs where applicable. Do not copy a load value or weather rating from another project. The local authority, structural professional and process owner should define the governing criteria and the conditions under which the enclosure must be closed, evacuated or taken out of service.
For controlled manufacturing overflow enclosure planning, condensation, solar gain, dust and rain entry should be treated as separate questions. State measurable environmental limits and monitoring locations; the word clean must not substitute for a qualified process specification. State which condition is merely uncomfortable and which one could invalidate maintenance, damage inventory or compromise evidence.
How to specify a clean manufacturing overflow tent
Define clear space, access and structure
The technical schedule should state span, length, eave and ridge height, bay spacing, clear openings and any zones where columns, bracing or anchors are prohibited. Show zones, flows, air-system boundaries, cleaning access, equipment, quarantine, utilities and emergency routes on one controlled drawing. Draw the asset and handling equipment at scale inside the proposed frame, including doors in their least favorable usable position.
Select the envelope and utility interfaces
Specify what the envelope must accomplish: provide cleanable specified interior surfaces and sealed interfaces compatible with the owner-designed environmental system. Name the membrane and frame references, joining method, replaceable wear parts, door hardware, floor interface and required finish. Avoid undefined terms such as “all-weather,” “clean,” “insulated” or “heavy duty” unless the RFQ states a test method and acceptance condition.
Utilities require a separate schedule. For the controlled manufacturing overflow enclosure, consider qualified filtration or HVAC, power, data, compressed services, lighting, monitoring and alarms. Show entry points, isolation locations, routing clearances and ownership. The enclosure manufacturer should not guess electrical capacity, extraction performance, process temperature or hazardous-area classification.
Measure the project instead of relying on labels
The following fields make quotes more comparable. The buyer should enter project-specific values rather than accept generic defaults:
- Process equipment and maintenance envelopes in millimetres.
- Owner-defined particle or cleanliness limits with test method.
- Temperature and humidity operating ranges.
- Pressure relationships in pascals where designed.
- Air-system duty in cubic metres per hour.
- Cleaning and environmental-monitoring frequencies.
Record the source, date and owner of each value. If a field is unknown, mark it “open” and state who will close it before design release. A blank technical assumption must not quietly become a supplier assumption.
Safety, compliance and evidence boundaries
Treat the tent as one part of a controlled system
The central hazard for this application is moving a controlled process into a temporary facility without validating contamination, utilities, emergency systems and worker protection. The owner’s risk assessment should cover access control, emergency routes, lighting, housekeeping, isolation, vehicle movement and weather response. Where hot work, hazardous energy, chemicals, food, medical products, evidence or regulated cargo are involved, the appropriate specialist must approve the operating controls.
An enclosure can improve weather protection, but it can also trap exhaust, heat, vapour or dust. Higher air change or tighter sealing can affect doors, pressure, temperature and emergency response. The facility and process designs must be reviewed together. Ventilation openings alone are not proof of safe air quality. Define the contaminant, source rate, monitoring method, alarm response and responsible person before selecting fans or closing panels.
Use official guidance without overclaiming
OSHA’s semiconductor manufacturing fact sheet shows the breadth of engineered controls used in contamination-sensitive high-technology production. Review OSHA semiconductor manufacturing safety fact sheet when preparing the operational brief. NIST describes quality systems as organized structures for controlling processes, responsibilities and documented information. The NIST Quality System guidance provides a second reference for the process owner.
Compare configurations on a complete scope
Evaluate three workable approaches
A useful comparison for the controlled manufacturing overflow enclosure includes:
- Basic weather shell: a cleanable protected store for sealed materials outside the production classification
- Process-support enclosure: a monitored assembly enclosure with owner-designed air treatment and formal qualification
- Phased or relocatable system: a phased modular suite with separate transfer, process and support zones for a temporary campaign
Challenge supplier assumptions
Ask each bidder to provide an inclusion-and-exclusion schedule, drawing list, proposed material references, design responsibility statement and evidence register. For the controlled manufacturing overflow enclosure, specifically challenge classification claims, liner materials, seams, pressure, air-system loads, transfer interfaces, cleaning, validation and restoration after removal. Require written review before any post-approval substitution.
Factory review and shipment inspection
Convert the approved design into checkable hold points
A practical sequence is requirement brief, site survey, concept layout, design review, first-article detail, production release, factory inspection, packing release, installation and site acceptance. For the controlled manufacturing overflow enclosure, the first-article detail should focus on one liner corner, floor transition, sealed service opening and transfer door. Approve it before repeating the feature across the batch.
In TentDawn’s Shenzhen production setting, an order-specific inspection plan can cover liner reference, seams, floor interface, door seals, penetrations, labels, protected packing and trial assembly of the first article. This describes useful controls, not completed checks for an unspecified order. The buyer should approve sampling, tolerances, records and witness points before manufacturing starts.
Pack for identification and installation sequence
Shipment inspection should reconcile the approved bill of materials with labelled packages. Use clean packs for interior-facing parts and a documented sequence that prevents construction hardware and dirty packaging entering the finished zone. Photograph agreed checkpoints, protect vulnerable edges and hardware, and separate site-supplied items from factory-supplied items on the packing list.
Installation preparation and site acceptance
Prepare the site before the delivery team arrives
Before dispatch, confirm segregated laydown, dust controls, liner protection, utility readiness, cleaning plan, commissioning instruments and quality release. Hold a coordination review with the owner, installer, structural reviewer and utility or process specialists. Resolve drawing revisions, access windows, permits, lifting plans and weather limits while changes are still manageable.
Commission the complete operating arrangement
Site acceptance for the controlled manufacturing overflow enclosure should demonstrate surface condition, flows, door operation, environmental-system testing, monitoring, cleaning verification and process-owner approval. Test representative flows with the actual or dimensionally equivalent equipment where safe. Record results, responsible people, open items and closeout dates instead of relying on a visual walk-through.
Cost, lead time and lifecycle planning
Identify the real price drivers
The main cost drivers are lining, floor, air treatment, transfer zones, utilities, commissioning, cleaning, monitoring and restoration of the host facility. Ask suppliers to separate base structure, options, engineering, freight, installation support and destination work. This makes value engineering visible and prevents a cheaper quote from winning only because it omits a necessary interface.
Plan inspection, cleaning and change control
Create a periodic inspection schedule for liner integrity, seals, floor transitions, filters by owner plan, monitoring points, doors and any contamination deviation. Frequency should respond to actual exposure, usage, manufacturer instructions and local requirements. Keep records of findings and corrective action; inspect after exceptional wind, snow, impact, relocation or unauthorized modification.
Internal TentDawn resources
Continue the procurement journey with food packaging overflow tent guide, mobile calibration laboratory tent guide, custom tent drawing approval guide. These guides address adjacent site, engineering, logistics and handover decisions without duplicating this article’s primary intent.
Procurement worksheet
- Define the operation, asset, duration and failure consequence.
- Attach a dimensioned plan showing movements, exits and installation zones.
- Record weather, ground, drainage and environmental inputs with sources.
- List utilities, process systems and their responsible designers.
- Identify applicable rules, reviewers, permits and approval dates.
- State clear dimensions and worst-case operating envelopes.
- Approve materials, drawings, interfaces and substitution controls.
- Define factory inspection, shipment release and packing evidence.
- Write site installation hold points and acceptance demonstrations.
- Assign maintenance, weather response and change-control ownership.
FAQ
Is a clean manufacturing tent automatically a cleanroom?
No. A cleanroom classification requires defined test methods, qualified air systems, materials, cleaning, monitoring and operating controls. The enclosure is only one component of a validated facility.
Which process should move into overflow space?
Choose a bounded process with known equipment, environmental needs, material flow and quality risks. Avoid moving an operation merely because floor area is available; assess contamination and validation impact first.
How should personnel and materials enter?
Use a process-approved flow that prevents cross-traffic and preserves required status. Separate personnel, incoming materials, released output and waste where the risk assessment requires it.
What should a first article include?
Mock up the most sensitive liner seam, floor junction, door and service penetration. Clean and inspect it using the intended method before approving repeated construction.
When is revalidation required?
Follow the owner’s quality system. Changes to product, process, equipment, utilities, airflow, materials or layout can trigger review and requalification before continued use.
Conclusion
A dependable clean manufacturing overflow tent begins with a controlled operating brief, verified site inputs and measurable acceptance evidence. For the controlled manufacturing overflow enclosure, the buyer should prioritize process definition, qualified utilities, controlled flows and quality validation. The best proposal is not the one with the broadest adjectives; it is the one whose assumptions, geometry, materials, responsibilities and records can be checked.
Mid-article CTA
Need a focused technical discussion? Send Your Requirements with the operation, asset dimensions, quantity, destination and target schedule. TentDawn can use that information to prepare the next specification questions.
Final CTA
Ready to compare a custom configuration? Get a Quote and request a drawing, material options, inspection plan, packing scope and clearly stated exclusions for your project.
START A PROJECT
Send us the basics.
We will reply with the right next questions for your custom tent requirement.